IoT Integration: Boosting US Manufacturing Efficiency by 15% in 2026
Anúncios
The manufacturing landscape in the United States is undergoing a profound transformation. Faced with global competition, rising operational costs, and an increasing demand for customized products, U.S. manufacturers are constantly seeking innovative ways to enhance productivity and efficiency. One of the most potent catalysts for this evolution is the Internet of Things (IoT). By 2026, the strategic integration of IoT into existing U.S. manufacturing facilities is projected to unlock an impressive 15% more efficiency, a significant leap that can redefine competitive advantage. But how exactly can this be achieved, particularly when dealing with established infrastructure and processes? This comprehensive guide delves into practical solutions for integrating IoT into existing U.S. manufacturing, outlining the benefits, challenges, and a strategic roadmap for success. The journey towards enhanced IoT Manufacturing Efficiency is not merely about adopting new technology; it’s about reimagining operational paradigms, fostering a data-driven culture, and empowering the workforce with actionable insights.
The Imperative for IoT Manufacturing Efficiency in the U.S.
The U.S. manufacturing sector, a cornerstone of the national economy, faces unique pressures. A skilled labor shortage, aging infrastructure, and the need for greater agility in supply chains are just a few of the hurdles. IoT offers a compelling answer to these challenges by providing unprecedented visibility and control over manufacturing processes. Imagine a factory where every machine, every tool, and every product can communicate in real-time, providing a constant stream of data that can be analyzed to identify bottlenecks, predict failures, and optimize performance. This is the promise of IoT, and its realization is critical for U.S. manufacturers aiming to maintain and grow their global standing.
The 15% efficiency gain is not an arbitrary figure. It represents a conservative estimate based on the cumulative impact of various IoT applications across different facets of manufacturing. This includes reductions in downtime due to predictive maintenance, optimized energy consumption, improved quality control through real-time monitoring, and enhanced supply chain visibility. For many manufacturers, even a 5% improvement can translate into millions of dollars in savings and increased revenue. The ambitious target of 15% underscores the transformative potential of a holistic IoT strategy, one that integrates seamlessly with existing operations rather than requiring a complete overhaul.
Anúncios
Defining IoT in the Manufacturing Context
At its core, the Internet of Things in manufacturing, often referred to as the Industrial Internet of Things (IIoT), involves the networking of physical devices, vehicles, home appliances, and other items embedded with electronics, software, sensors, actuators, and network connectivity that enables these objects to collect and exchange data. In a factory setting, this means connecting machinery, production lines, inventory systems, and even individual products to a central network. The data collected from these connected devices provides a granular view of operations, enabling data-driven decision-making that was previously impossible. This real-time data is the fuel for achieving significant IoT Manufacturing Efficiency gains.
Key components of an IIoT ecosystem include:
- Sensors and Actuators: These are the eyes and hands of the IIoT, collecting data on temperature, pressure, vibration, machine status, and more, or performing actions based on instructions.
- Connectivity: Secure and reliable networks (Wi-Fi, Ethernet, 5G, LPWAN) to transmit data from devices to the cloud or edge computing platforms.
- Data Processing and Analytics: Software platforms that ingest, process, and analyze vast amounts of data, often leveraging artificial intelligence (AI) and machine learning (ML) to extract actionable insights.
- User Interfaces and Dashboards: Tools that present complex data in an understandable format, allowing operators and managers to monitor performance and make informed decisions.
- Cloud and Edge Computing: Infrastructure for storing and processing data, with edge computing offering localized processing for faster response times and reduced bandwidth usage.
Practical Solutions for Integrating IoT into Existing Manufacturing
Integrating IoT into a brand-new, purpose-built factory is one thing; retrofitting it into an existing facility with decades-old machinery and established workflows presents a different set of challenges. However, it is precisely in these existing environments where the most significant and immediate gains in IoT Manufacturing Efficiency can be realized. The key lies in a phased, strategic approach that prioritizes quick wins and demonstrates tangible ROI.
Anúncios
1. Non-Invasive Sensor Deployment and Retrofitting
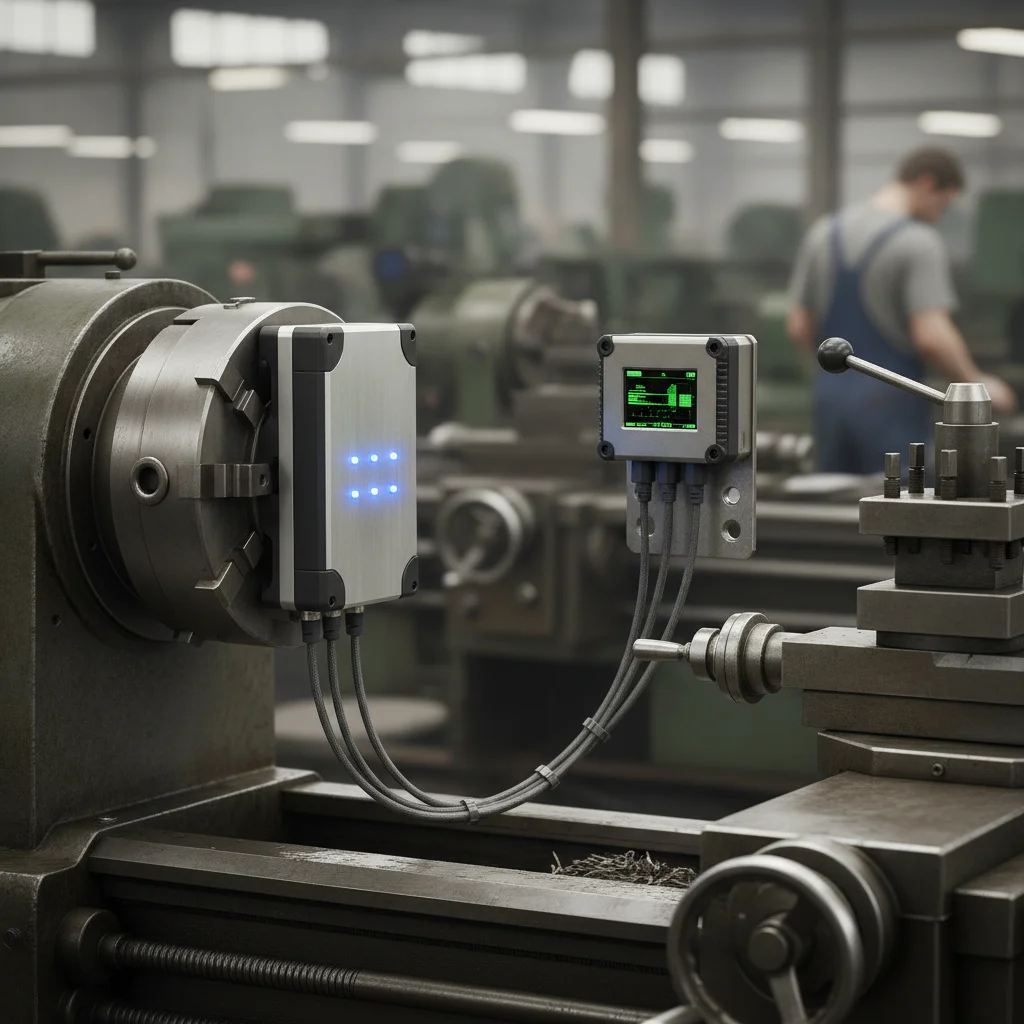
One of the primary concerns for manufacturers with legacy equipment is the cost and complexity of replacing functional machinery. Fortunately, many IoT solutions are designed for non-invasive deployment. This involves adding external sensors to existing machines without altering their core functionality. These sensors can monitor various parameters:
- Vibration Sensors: Attached to motors, pumps, and other rotating equipment to detect anomalies that indicate impending mechanical failure, enabling predictive maintenance.
- Temperature Sensors: Monitoring critical components to prevent overheating, ensure optimal operating conditions, and reduce energy waste.
- Acoustic Sensors: Listening for unusual sounds that could signify wear and tear or operational issues.
- Current/Voltage Sensors: Measuring power consumption of individual machines to identify inefficiencies and optimize energy usage.
- Proximity Sensors: Tracking the movement of parts, products, or even personnel on the factory floor to optimize workflow and safety.
Retrofitting also extends to connecting older programmable logic controllers (PLCs) and supervisory control and data acquisition (SCADA) systems to the IoT network through gateways. These gateways act as translators, converting proprietary industrial protocols into standard internet protocols, allowing legacy data to be integrated into modern analytics platforms. This approach significantly lowers the barrier to entry for IoT Manufacturing Efficiency.
2. Predictive Maintenance for Reduced Downtime
Perhaps the most immediate and impactful benefit of IoT in existing manufacturing is the shift from reactive or preventive maintenance to predictive maintenance. Instead of repairing equipment after it breaks down (reactive) or on a fixed schedule (preventive), predictive maintenance uses real-time data from sensors to anticipate failures before they occur. This is a cornerstone of achieving 15% more IoT Manufacturing Efficiency.
By continuously monitoring machine health, algorithms can detect subtle changes in vibration, temperature, or current draw that signal an impending issue. This allows maintenance teams to schedule interventions precisely when needed, minimizing unplanned downtime, optimizing resource allocation, and extending the lifespan of valuable assets. For example, a sensor might detect a slight increase in motor vibration, triggering an alert that allows technicians to replace a bearing during a scheduled break rather than waiting for the motor to seize up during peak production.
3. Real-time Production Monitoring and Optimization
IoT provides an unparalleled level of visibility into the production process. Sensors on conveyor belts, assembly lines, and individual workstations can track progress, identify bottlenecks, and measure key performance indicators (KPIs) in real-time. This includes:
- Overall Equipment Effectiveness (OEE): A crucial metric that combines availability, performance, and quality. IoT systems can automatically calculate OEE for each machine and line, providing instant insights into operational health.
- Cycle Time Analysis: Identifying variations in production cycles and pinpointing areas for process improvement.
- Scrap and Rework Rates: Real-time monitoring can detect quality issues earlier, reducing waste and the need for costly rework, thereby directly contributing to IoT Manufacturing Efficiency.
With this data, plant managers can make informed decisions to reallocate resources, adjust production schedules, and optimize workflows on the fly, leading to significant efficiency gains.
4. Energy Management and Sustainability
Manufacturing facilities are often significant consumers of energy. IoT-enabled energy management systems can monitor electricity, gas, and water consumption at a granular level – from the entire plant down to individual machines. This data allows manufacturers to:
- Identify Energy Hogs: Pinpoint machines or processes that consume excessive energy.
- Optimize Usage: Schedule operations for off-peak hours or automatically power down idle equipment.
- Detect Leaks and Waste: Monitor utility lines for anomalies that indicate leaks or inefficient usage.
Beyond cost savings, optimized energy consumption contributes to the manufacturer’s sustainability goals, enhancing their brand image and compliance with environmental regulations. This dual benefit further reinforces the value proposition of IoT Manufacturing Efficiency.
5. Supply Chain Integration and Inventory Management
IoT extends beyond the factory floor to integrate with the broader supply chain. Smart sensors and RFID tags can track raw materials from suppliers, through production, and to the final customer. This provides:
- Real-time Inventory Visibility: Knowing the exact location and quantity of materials and finished goods, reducing the need for buffer stock and preventing stockouts.
- Automated Reordering: Triggering orders for materials when stock levels fall below a predefined threshold, optimizing inventory turnover.
- Improved Logistics: Tracking shipments and optimizing routes, reducing transportation costs and delivery times.
By streamlining the supply chain, manufacturers can reduce lead times, cut carrying costs, and respond more agilely to market demands, all contributing to overall IoT Manufacturing Efficiency.
Challenges and Mitigation Strategies for Existing Facilities
While the benefits are clear, integrating IoT into existing U.S. manufacturing facilities is not without its hurdles. These often include:
- Legacy Infrastructure: Older machines may lack digital interfaces, requiring specialized sensors and gateways.
- Data Silos: Information often resides in disparate systems (SCADA, MES, ERP) that don’t communicate with each other.
- Cybersecurity Concerns: Connecting operational technology (OT) to IT networks creates new vulnerabilities.
- Skills Gap: A shortage of personnel with expertise in IoT, data analytics, and cybersecurity.
- Cost of Implementation: Initial investment in sensors, software, and infrastructure.
- Resistance to Change: Employees may be hesitant to adopt new technologies and workflows.
Mitigation Strategies:
- Phased Implementation: Start with pilot projects that target specific pain points and offer clear, measurable ROI. This builds confidence and demonstrates value.
- Open Standards and Protocols: Prioritize IoT solutions that support open standards to ensure interoperability between new and existing systems.
- Robust Cybersecurity Framework: Implement a layered security approach, including network segmentation, encryption, access controls, and regular vulnerability assessments.
- Workforce Training and Upskilling: Invest in training programs to equip existing employees with the skills needed to operate and maintain IoT systems.
- Partnerships with IoT Providers: Collaborate with experienced IoT vendors who offer solutions tailored for brownfield sites and provide ongoing support.
- Change Management: Actively communicate the benefits of IoT to employees, involve them in the implementation process, and address their concerns to foster adoption.
The Roadmap to 15% More IoT Manufacturing Efficiency by 2026
Achieving a 15% efficiency boost by 2026 requires a well-defined strategy. Here’s a typical roadmap:
Phase 1: Assessment and Planning (6-12 Months)
- Identify Pain Points and Opportunities: Conduct a comprehensive audit of current operations to pinpoint areas with high potential for IoT impact (e.g., frequent machine breakdowns, high energy consumption, inventory inaccuracies).
- Define Clear Objectives and KPIs: Establish specific, measurable, achievable, relevant, and time-bound (SMART) goals for IoT implementation, directly linked to IoT Manufacturing Efficiency.
- Technology Stack Selection: Research and select appropriate IoT platforms, sensors, gateways, and analytics tools that are compatible with existing infrastructure.
- Build a Cross-Functional Team: Assemble a team comprising IT, OT, operations, and maintenance personnel to steer the project.
- Develop a Cybersecurity Strategy: Integrate security considerations from the outset.
Phase 2: Pilot Implementation (3-6 Months)
- Start Small: Implement IoT in a specific, contained area or on a critical piece of equipment. This allows for testing, learning, and refining the approach without disrupting the entire operation.
- Data Collection and Validation: Begin collecting data and ensure its accuracy and reliability.
- Initial Analytics and Insights: Use basic analytics to identify early trends and validate the chosen solutions.
- Measure ROI: Quantify the benefits achieved during the pilot phase to build a strong business case for broader deployment.
Phase 3: Scaled Deployment and Integration (12-24 Months)
- Expand Scope: Gradually roll out IoT solutions across more machines, production lines, and departments based on the lessons learned from the pilot.
- Integrate with Enterprise Systems: Connect IoT data with existing ERP, MES, and CMMS systems to create a unified view of operations.
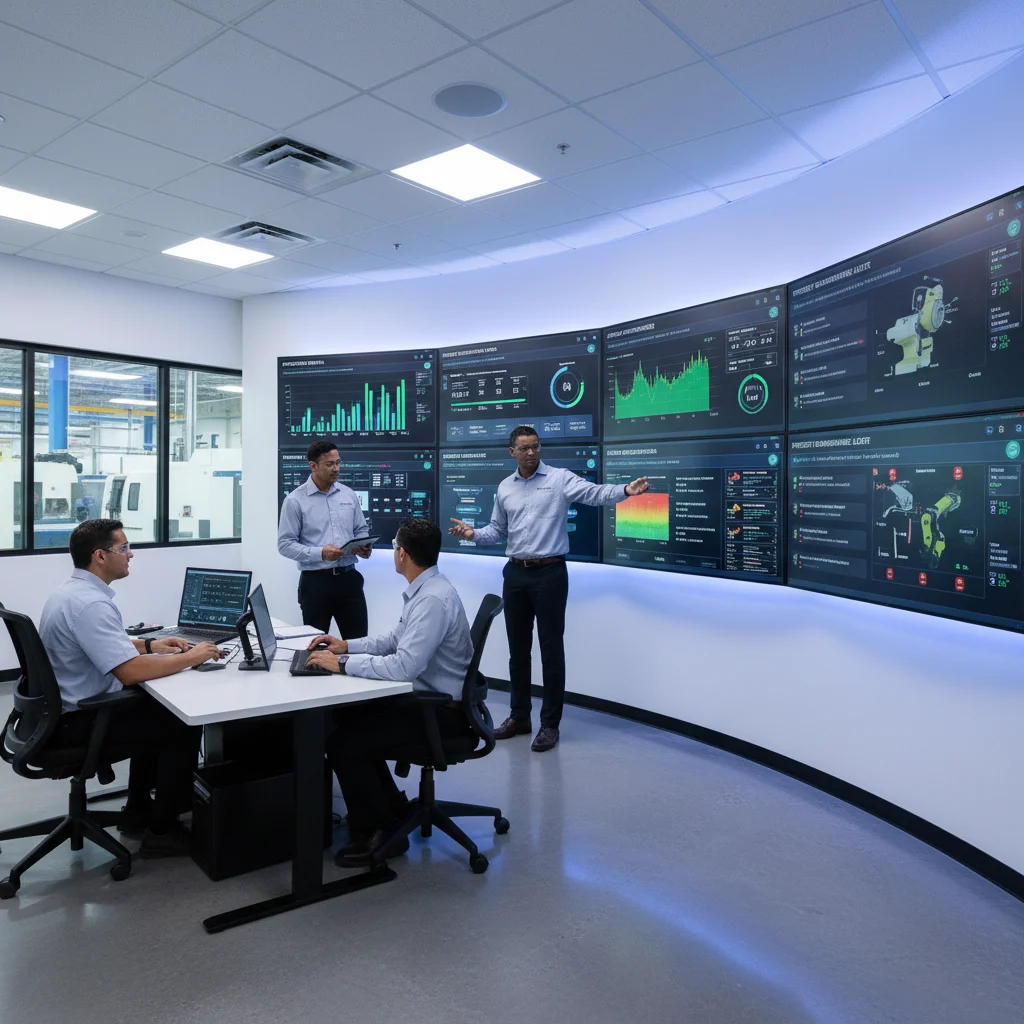
- Advanced Analytics and AI/ML: Implement more sophisticated analytics, including machine learning models for predictive maintenance, quality control, and demand forecasting. These advanced capabilities are crucial for maximizing IoT Manufacturing Efficiency.
- Workforce Empowerment: Provide ongoing training and tools to empower employees to leverage IoT data for their daily tasks.
Phase 4: Continuous Optimization and Innovation (Ongoing)
- Performance Monitoring: Continuously monitor IoT system performance and its impact on key efficiency metrics.
- Feedback Loop: Establish mechanisms for feedback from operators and engineers to identify new opportunities for improvement.
- Stay Abreast of New Technologies: Regularly evaluate emerging IoT technologies and trends to ensure the manufacturing facility remains at the forefront of innovation.
The Human Element: Empowering the Workforce
While technology is a critical enabler, the success of IoT integration hinges on the human element. The fear of automation leading to job displacement is a common concern. However, in the context of IoT Manufacturing Efficiency, the goal is not to replace human workers but to augment their capabilities. IoT transforms roles, creating new opportunities for skilled technicians, data analysts, and system integrators.
For example, instead of performing routine, time-based maintenance, technicians can become proactive problem-solvers, interpreting data to diagnose issues before they escalate. Production line workers can gain real-time insights into their output and quality, allowing them to make immediate adjustments. This shift requires investment in reskilling and upskilling the existing workforce, transforming them into digital-savvy operators and decision-makers. Companies that prioritize this human-centric approach will not only achieve greater efficiency but also foster a more engaged and empowered workforce.
Future Outlook: Beyond 2026
The 15% efficiency gain by 2026 is just the beginning. As IoT technology matures and integrates further with other Industry 4.0 pillars like Artificial Intelligence (AI), Machine Learning (ML), and Digital Twins, the potential for even greater gains will emerge. Factories will become increasingly autonomous, self-optimizing, and resilient. Predictive analytics will evolve into prescriptive analytics, not just predicting problems but recommending specific actions to prevent them.
The U.S. manufacturing sector has an opportunity to lead this global digital transformation. By embracing IoT now, focusing on practical, scalable solutions for existing infrastructure, and investing in its people, American manufacturers can not only achieve significant efficiency improvements but also build a more robust, competitive, and sustainable future. The journey towards enhanced IoT Manufacturing Efficiency is a continuous one, promising a future where data-driven insights power every aspect of production, leading to unprecedented levels of productivity and innovation.
Conclusion
Integrating IoT into existing U.S. manufacturing facilities by 2026 is not merely an option but a strategic imperative for unlocking 15% more efficiency. This significant improvement is achievable through a combination of non-invasive sensor deployment, robust predictive maintenance strategies, real-time production monitoring, intelligent energy management, and seamless supply chain integration. While challenges such as legacy infrastructure and cybersecurity exist, they can be effectively mitigated through phased implementation, strategic partnerships, and a strong focus on workforce development.
The roadmap outlined above provides a clear path for manufacturers to embark on this transformative journey. By embracing a data-driven culture and empowering their employees, U.S. manufacturers can leverage the power of IoT to enhance their competitiveness, reduce operational costs, and drive sustainable growth. The future of American manufacturing is undeniably connected, intelligent, and highly efficient, and the time to act is now to secure a leading position in the global industrial landscape.
