7 Disruptive IoT Technologies Transforming US Manufacturing in 18 Months
Anúncios
The landscape of US manufacturing is on the precipice of a profound transformation, driven by an accelerating wave of technological innovation. At the heart of this revolution lies the Internet of Things (IoT), a network of interconnected devices, sensors, and software that are fundamentally reshaping how factories operate, products are made, and supply chains are managed. The next 18 months are critical, as several disruptive IoT technologies are set to move from nascent adoption to widespread integration, promising unprecedented levels of efficiency, productivity, and competitive advantage for those who embrace them. This article delves into the seven most impactful IoT Manufacturing Transformation technologies that will define the future of US manufacturing.
Understanding the IoT Manufacturing Transformation Paradigm
Before we dive into the specific technologies, it’s crucial to grasp the overarching concept of the IoT Manufacturing Transformation. It’s more than just connecting machines; it’s about creating an intelligent, self-optimizing ecosystem where every component, from raw materials to finished products, can communicate and collaborate. This paradigm shift enables manufacturers to gain real-time insights into their operations, predict potential issues before they arise, and adapt quickly to changing market demands. The stakes are high, and the rewards for successful adoption are immense, including reduced operational costs, improved product quality, faster time-to-market, and enhanced worker safety.
The journey towards a fully connected smart factory is iterative, but the foundational elements are already in place. Companies that invest in these disruptive IoT technologies today will be well-positioned to lead the next generation of industrial innovation. The competitive pressure from global markets, coupled with the need for greater resilience and agility in supply chains, makes the adoption of these technologies not just an advantage, but a necessity for sustained growth in the US manufacturing sector.
Anúncios
The Driving Forces Behind IoT Adoption in Manufacturing
Several factors are accelerating the adoption of IoT in manufacturing. Firstly, the decreasing cost of sensors and connectivity makes these technologies more accessible to a wider range of businesses, including small and medium-sized enterprises (SMEs). Secondly, advancements in data analytics and artificial intelligence (AI) are enabling manufacturers to extract meaningful insights from the vast amounts of data generated by IoT devices. This data-driven approach empowers better decision-making and continuous process improvement. Thirdly, the increasing demand for customized products and shorter product lifecycles necessitates more flexible and responsive production systems, which IoT can deliver. Finally, the ongoing labor shortage in manufacturing is driving the need for automation and intelligent systems that can augment human capabilities and optimize resource allocation.
1. Advanced Predictive Maintenance Systems
One of the most immediate and impactful applications of IoT in manufacturing is advanced predictive maintenance. Traditionally, maintenance has been either reactive (fixing things when they break) or preventive (scheduled maintenance regardless of actual need). Predictive maintenance, powered by IoT sensors, shifts this paradigm entirely. Sensors embedded in machinery continuously monitor performance parameters such as vibration, temperature, pressure, and acoustics. This data is then analyzed by AI algorithms to detect anomalies and predict potential equipment failures long before they occur.
The disruption here is profound. Instead of costly unscheduled downtime, manufacturers can schedule maintenance proactively during planned breaks, order parts just-in-time, and extend the lifespan of their assets. This leads to significant cost savings, increased operational uptime, and a more predictable production schedule. Within the next 18 months, we will see a widespread shift from traditional maintenance approaches to sophisticated predictive models, becoming a cornerstone of efficient factory operations. The ROI on these systems is often rapid, making them a top priority for manufacturers looking to optimize their capital expenditures and operational efficiency.
Anúncios
Consider a scenario where a critical machine component shows subtle signs of wear. Without predictive maintenance, this might go unnoticed until a catastrophic failure, leading to hours or even days of production loss. With IoT-enabled predictive maintenance, sensors detect the minute deviations from normal operating parameters. AI algorithms analyze this data, comparing it against historical patterns and machine learning models, and then trigger an alert. Maintenance teams receive precise information about which component is failing, what kind of repair is needed, and how much time they have before an actual breakdown. This allows them to schedule maintenance during a non-production shift, order the specific part needed, and minimize disruption. The result is a seamless operation, reduced maintenance costs, and a significant boost in overall equipment effectiveness (OEE).
2. Real-time Asset Tracking and Management
In complex manufacturing environments, knowing the exact location and status of every asset – from raw materials and work-in-progress to tools and finished goods – is a monumental challenge. IoT-enabled real-time asset tracking and management solutions are set to revolutionize this aspect. By deploying RFID tags, Bluetooth Low Energy (BLE) beacons, and GPS sensors, manufacturers can gain unprecedented visibility into their entire inventory and equipment movements.
This technology eliminates lost or misplaced items, reduces search times, and optimizes material flow on the factory floor and across the supply chain. It also provides valuable data for optimizing warehouse layouts, identifying bottlenecks, and improving overall logistics. The ability to monitor environmental conditions for sensitive materials (e.g., temperature, humidity) further enhances quality control. In the coming months, expect to see widespread adoption of these systems, moving beyond simple inventory management to intelligent, dynamic asset orchestration. The immediate benefits include reduced operational overhead, improved inventory accuracy, and enhanced supply chain resilience.
Imagine a large automotive assembly plant where thousands of parts move through various stages of production daily. Without real-time tracking, locating a specific batch of components or a critical tool can be a time-consuming and frustrating task, leading to delays and inefficiencies. With IoT asset tracking, each component, tool, and even automated guided vehicle (AGV) is tagged with a sensor. Gateways and readers strategically placed throughout the facility collect data on their location and movement. This information is fed into a central dashboard, providing a live map of the entire operation. If a specific part is needed, its exact location can be pinpointed instantly. If a tool is missing, its last known location is readily available. This level of granular visibility not only saves time but also prevents production stoppages due to missing items, optimizes the utilization of expensive tools, and ensures that materials are always where they need to be, precisely when they are needed.
3. Industrial IoT (IIoT) Platforms and Edge Computing
The sheer volume of data generated by IoT devices in a manufacturing setting can be overwhelming. Industrial IoT (IIoT) platforms are designed to collect, process, analyze, and visualize this data, providing a centralized hub for operational intelligence. Coupled with edge computing, which processes data closer to its source (i.e., on the factory floor rather than in a distant cloud), these platforms enable real-time decision-making and reduce latency.
The disruptive aspect lies in their ability to transform raw data into actionable insights, empowering operators and managers to optimize processes, identify inefficiencies, and respond to incidents almost instantaneously. Edge computing is particularly crucial for applications requiring ultra-low latency, such as controlling robotic arms or ensuring safety protocols. Over the next 18 months, the integration of robust IIoT platforms with powerful edge computing capabilities will become standard, forming the backbone of smart factories and driving the IoT Manufacturing Transformation. These platforms also provide the necessary security infrastructure to protect sensitive operational data from cyber threats.
Consider a scenario in a high-speed packaging plant. Hundreds of sensors on various machines generate gigabytes of data every minute. Sending all this data to a remote cloud for processing introduces latency, which can be critical if an immediate adjustment is needed to prevent a defect or machine malfunction. With an IIoT platform leveraging edge computing, a significant portion of this data is processed locally, right at the factory floor. Edge devices can filter out redundant data, perform initial analytics, and trigger immediate alerts or even autonomous machine adjustments in milliseconds. Only aggregated or critical data is then sent to the cloud for deeper, long-term analysis and historical trending. This hybrid approach ensures both rapid response times for critical operations and comprehensive data insights for strategic planning, creating a truly responsive and intelligent manufacturing environment.
4. Digital Twins for Process Optimization
Digital Twins are virtual replicas of physical assets, processes, or even entire factory layouts. These dynamic models are fed real-time data from IoT sensors, allowing manufacturers to simulate, analyze, and predict the behavior of their physical counterparts. This technology offers an unparalleled level of insight into operational performance without disrupting actual production.
The disruptive power of Digital Twins lies in their ability to enable ‘what-if’ scenarios, optimize production lines, test new product designs, and even train operators in a risk-free virtual environment. They facilitate continuous improvement by identifying potential bottlenecks, predicting maintenance needs, and optimizing energy consumption. Within the next year and a half, Digital Twins will become indispensable tools for design, engineering, and operations teams, significantly accelerating innovation and efficiency within the IoT Manufacturing Transformation journey. Their ability to provide a comprehensive, real-time view of complex systems makes them a cornerstone for advanced decision support.
Imagine a manufacturer planning to reconfigure a complex assembly line to produce a new product variant. Traditionally, this would involve extensive physical trials, which are costly, time-consuming, and carry the risk of disrupting existing production. With a Digital Twin of the assembly line, engineers can create a virtual model of the new configuration. They can then simulate the flow of materials, the movement of robots, and the timing of each process step, all in a virtual environment. Real-time data from the existing factory can be fed into the Digital Twin to ensure its accuracy. They can identify potential bottlenecks, optimize robot paths, and even predict the impact of various scheduling changes, all before making any physical modifications. This allows them to refine the new line configuration, test different scenarios, and train operators virtually, drastically reducing the time and cost associated with physical implementation and ensuring a smooth transition to new production.
5. Augmented Reality (AR) for Enhanced Workforce Productivity
While often associated with consumer applications, Augmented Reality (AR) is rapidly emerging as a transformative tool in manufacturing, particularly when combined with IoT data. AR overlays digital information onto the real-world view, providing workers with context-sensitive data, step-by-step instructions, and remote assistance directly within their field of vision.
This technology is disrupting traditional training methods, maintenance procedures, and quality control processes. Technicians can use AR glasses to visualize IoT data from a machine, receive interactive repair guides, or connect with remote experts who can see exactly what they see. This reduces errors, speeds up task completion, and significantly lowers training costs. As manufacturing grapples with an aging workforce and a skills gap, AR, integrated with IoT, offers a powerful solution to empower the next generation of workers and enhance the capabilities of existing teams. Expect to see AR becoming a common tool on factory floors within the next 18 months, driving significant gains in productivity and reducing human error.
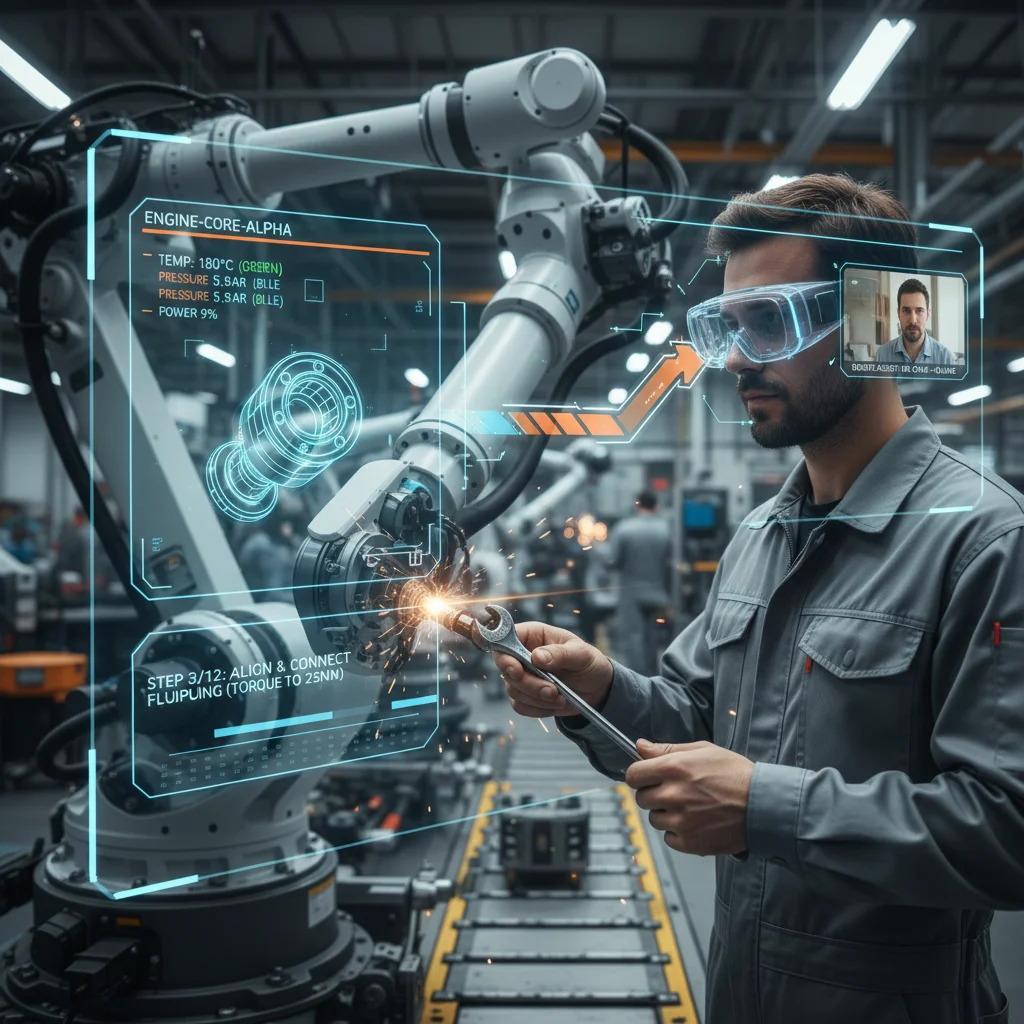
Consider a new employee tasked with performing a complex maintenance procedure on a piece of machinery they are unfamiliar with. Instead of relying solely on a thick manual or a supervisor’s verbal instructions, they don AR glasses. As they look at the machine, the AR system overlays digital labels identifying components, highlights the exact sequence of steps to follow, and even displays real-time diagnostic data from IoT sensors embedded in the machine. If they encounter an issue, they can instantly connect with a remote expert who can see their exact view and draw annotations or provide verbal guidance directly through the AR interface. This drastically reduces the learning curve, minimizes the risk of errors, and ensures that even complex tasks can be performed accurately and efficiently by less experienced personnel, thereby accelerating the IoT Manufacturing Transformation by empowering the workforce.
6. AI-Powered Quality Control and Vision Systems
Traditional quality control in manufacturing often involves manual inspections or rule-based automated systems that can miss subtle defects. IoT, combined with Artificial Intelligence (AI) and advanced vision systems, is revolutionizing this critical area. High-resolution cameras, integrated with IoT networks, capture images and videos of products at various stages of production. AI algorithms then analyze this visual data in real-time to detect defects, inconsistencies, and deviations from quality standards with unprecedented accuracy and speed.
This disruptive technology can identify flaws invisible to the human eye, reduce rework, minimize scrap, and ensure consistent product quality across entire production runs. It moves quality control from a reactive process to a proactive one, catching issues early and preventing them from propagating further down the line. Within the next 18 months, AI-powered vision systems will be widely deployed in critical inspection points, significantly enhancing product quality and reducing warranty claims, thus solidifying their role in the IoT Manufacturing Transformation. This also allows for more detailed traceability of product quality throughout the entire manufacturing process.
Imagine a circuit board manufacturing line where even microscopic defects can lead to product failure. Manual inspection is slow and prone to human error, while traditional automated vision systems might struggle with subtle variations. An AI-powered quality control system uses high-resolution cameras to capture images of every circuit board as it moves down the line. These images are instantly fed to an AI model trained on thousands of examples of both perfect and defective boards. The AI can detect minute cracks, misaligned components, or soldering issues that a human eye might miss. If a defect is found, the system immediately flags the board, potentially even directing a robotic arm to remove it from the line. This real-time, highly accurate inspection ensures that only flawless products proceed, significantly reducing waste, improving reliability, and maintaining brand reputation. The continuous learning capability of AI means the system gets better at identifying new types of defects over time, making it an invaluable asset in maintaining high quality standards.
7. Smart Supply Chain Integration and Transparency
The modern supply chain is a complex web of interconnected entities, often lacking real-time visibility and prone to disruptions. IoT technologies are set to bring unprecedented transparency and intelligence to supply chain management, creating a truly smart and resilient ecosystem. By deploying IoT sensors on raw materials, components, and finished goods, manufacturers can track their journey from source to customer in real-time.
This includes monitoring location, environmental conditions (temperature, humidity for perishable goods), and even tampering. The disruption here is the ability to anticipate and mitigate supply chain risks, optimize logistics, reduce inventory holding costs, and provide customers with accurate delivery estimates. Smart contracts, powered by blockchain and triggered by IoT data, can further automate and secure transactions. Over the next 18 months, the integration of IoT across the supply chain will evolve from niche applications to a fundamental requirement for competitive manufacturing, ensuring greater agility and responsiveness in a volatile global market. This enhanced visibility also supports ethical sourcing and compliance initiatives.
Consider a pharmaceutical company transporting sensitive vaccines that require strict temperature control. Without smart supply chain integration, monitoring these conditions during transit is difficult, and any temperature excursion might only be discovered upon arrival, rendering the entire shipment unusable. With IoT-enabled smart supply chain integration, each container of vaccines is equipped with temperature and humidity sensors. These sensors transmit real-time data to a central platform. If the temperature deviates from the required range, immediate alerts are sent to logistics managers, allowing for intervention or rerouting. Furthermore, the IoT data can be integrated with blockchain-based smart contracts, automatically triggering payments or penalties based on predefined conditions (e.g., successful delivery within temperature limits). This level of transparency not only ensures product integrity but also provides end-to-end traceability, optimizes logistics routes, and builds greater trust among supply chain partners, driving a more efficient and resilient IoT Manufacturing Transformation.
The Road Ahead: Embracing the IoT Manufacturing Transformation
The seven disruptive IoT technologies discussed above are not isolated innovations; they are interconnected components of a larger, intelligent manufacturing ecosystem. Their combined power will lead to factories that are not only more efficient and productive but also more adaptable, sustainable, and resilient. The IoT Manufacturing Transformation is not a distant future; it is happening now, and the next 18 months will be a period of accelerated adoption and significant change for US manufacturers.
For businesses looking to thrive in this new era, the key is to develop a clear IoT strategy, identify pilot projects that can deliver quick wins, and invest in the necessary infrastructure and talent. This includes fostering a culture of data-driven decision-making and ensuring cybersecurity measures are robust enough to protect the interconnected systems. The benefits of embracing these technologies – from reduced operational costs and improved product quality to enhanced worker safety and increased competitive advantage – far outweigh the challenges of implementation.
Manufacturers who proactively adopt these disruptive IoT technologies will not only optimize their current operations but also unlock new business models, drive innovation, and solidify their position as leaders in the global market. The journey towards a fully digitized and interconnected manufacturing future is an exciting one, and the time to act is now. The ability to harness the power of real-time data and intelligent automation will be the defining characteristic of successful manufacturing enterprises in the coming years. This revolution demands a holistic approach, where technology, processes, and people are all aligned towards the common goal of creating smarter, more agile, and more efficient production systems. The future of manufacturing is intelligent, and IoT is its cornerstone.
